Canadian owned and operated.
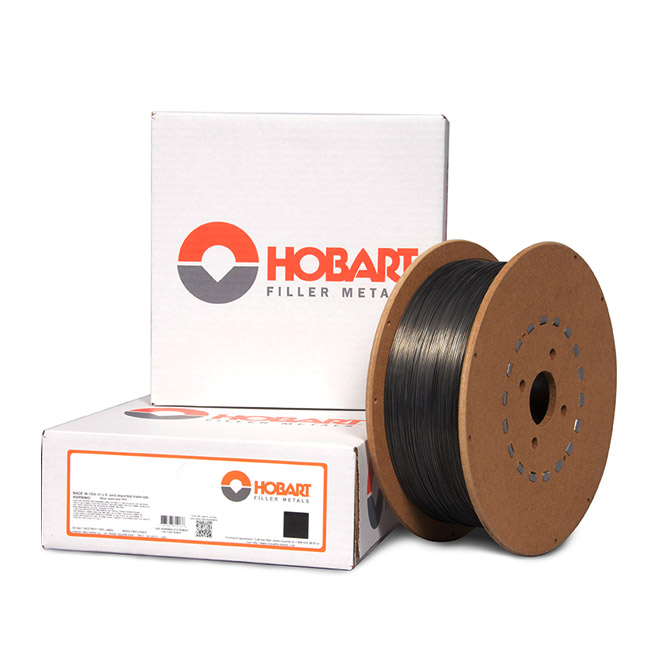
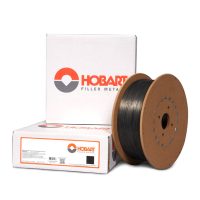
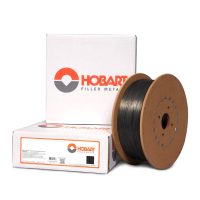
When your project involves welding quenched and tempered steels like T-1 or ASTM A514, standard welding wires simply won't cut it. You need a consumable that matches the base metal's superior yield strength and toughness. Enter the Hobart Fabco 110, a high-performance flux-cored wire engineered to deliver 110,000 psi tensile strength without compromising on weldability. This .045-inch wire is the go-to solution for fabricators building heavy earthmovers, crane booms, and critical structural components that must withstand immense stress and harsh environments.
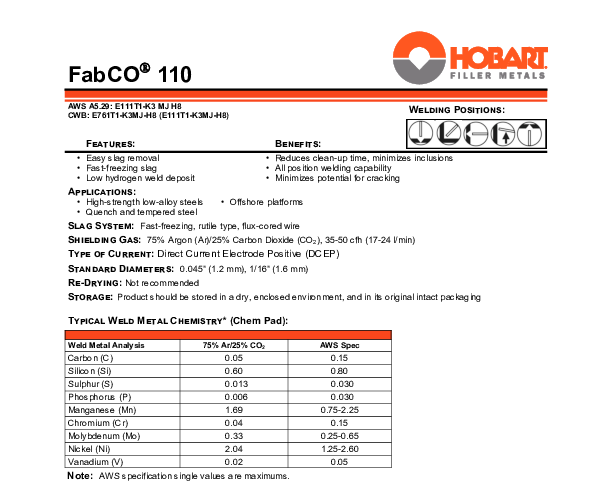
The primary challenge in welding high-strength steels is avoiding cracking, particularly in the heat-affected zone (HAZ). Fabco 110 addresses this with a sophisticated low-hydrogen formulation that significantly reduces the risk of underbead cracking. Furthermore, its nickel-alloyed chemistry provides exceptional impact toughness, even at temperatures as low as -40°F. This makes it an ideal choice for equipment operating in freezing climates or offshore applications where brittle fracture is a major concern.
Unlike some high-strength wires that are fluid and difficult to control out of position, Fabco 110 is designed with a fast-freezing slag. This characteristic allows welders to lay down high-quality beads in vertical and overhead positions with confidence. The puddle is controllable, and the arc remains consistent, allowing for precise penetration and bead contouring. Whether you are repairing a mining truck bed or fabricating a pressure vessel, this wire offers the versatility needed to tackle complex joint configurations.
To get the best performance out of Fabco 110, it is optimized for a 75% Argon / 25% CO2 shielding gas mix. This blend provides a smoother arc and better mechanical properties compared to straight CO2. The result is a cleaner weld with less spatter and better fusion. By choosing Hobart Fabco 110, you aren't just buying wire; you are investing in the structural reliability of your finished product.
| Additional Information |
|---|
| Brand:Hobart |
| Diameter:0.045 in |
| Packaging Description:33lb spool |
| Spool Size:33 lb Spool |
| Weld Process:Flux-Cored (FCAW) |
| Position:All Position |
| Polarity:DCEP |
| AWS Classification:E110T1-K3C, E111T1-K3M |
| Shielding Gas:75% Argon / 25% CO2 |
| Tensile Strength:110,000 psi (Typical) |
| Material Application:ASTM A514, HY-80, T-1 Steel |
| Diffusible Hydrogen:< 5.0 ml/100g |
| Item:flux-cored wire |
| AWS Spec:E110T1-K3C, E111T1-K3M |
No reviews yet
Nobody has rated this product yet. If you have run it on the job, yours is the review the next buyer reads.
Used this product on the job? Tell other welders how it held up.